

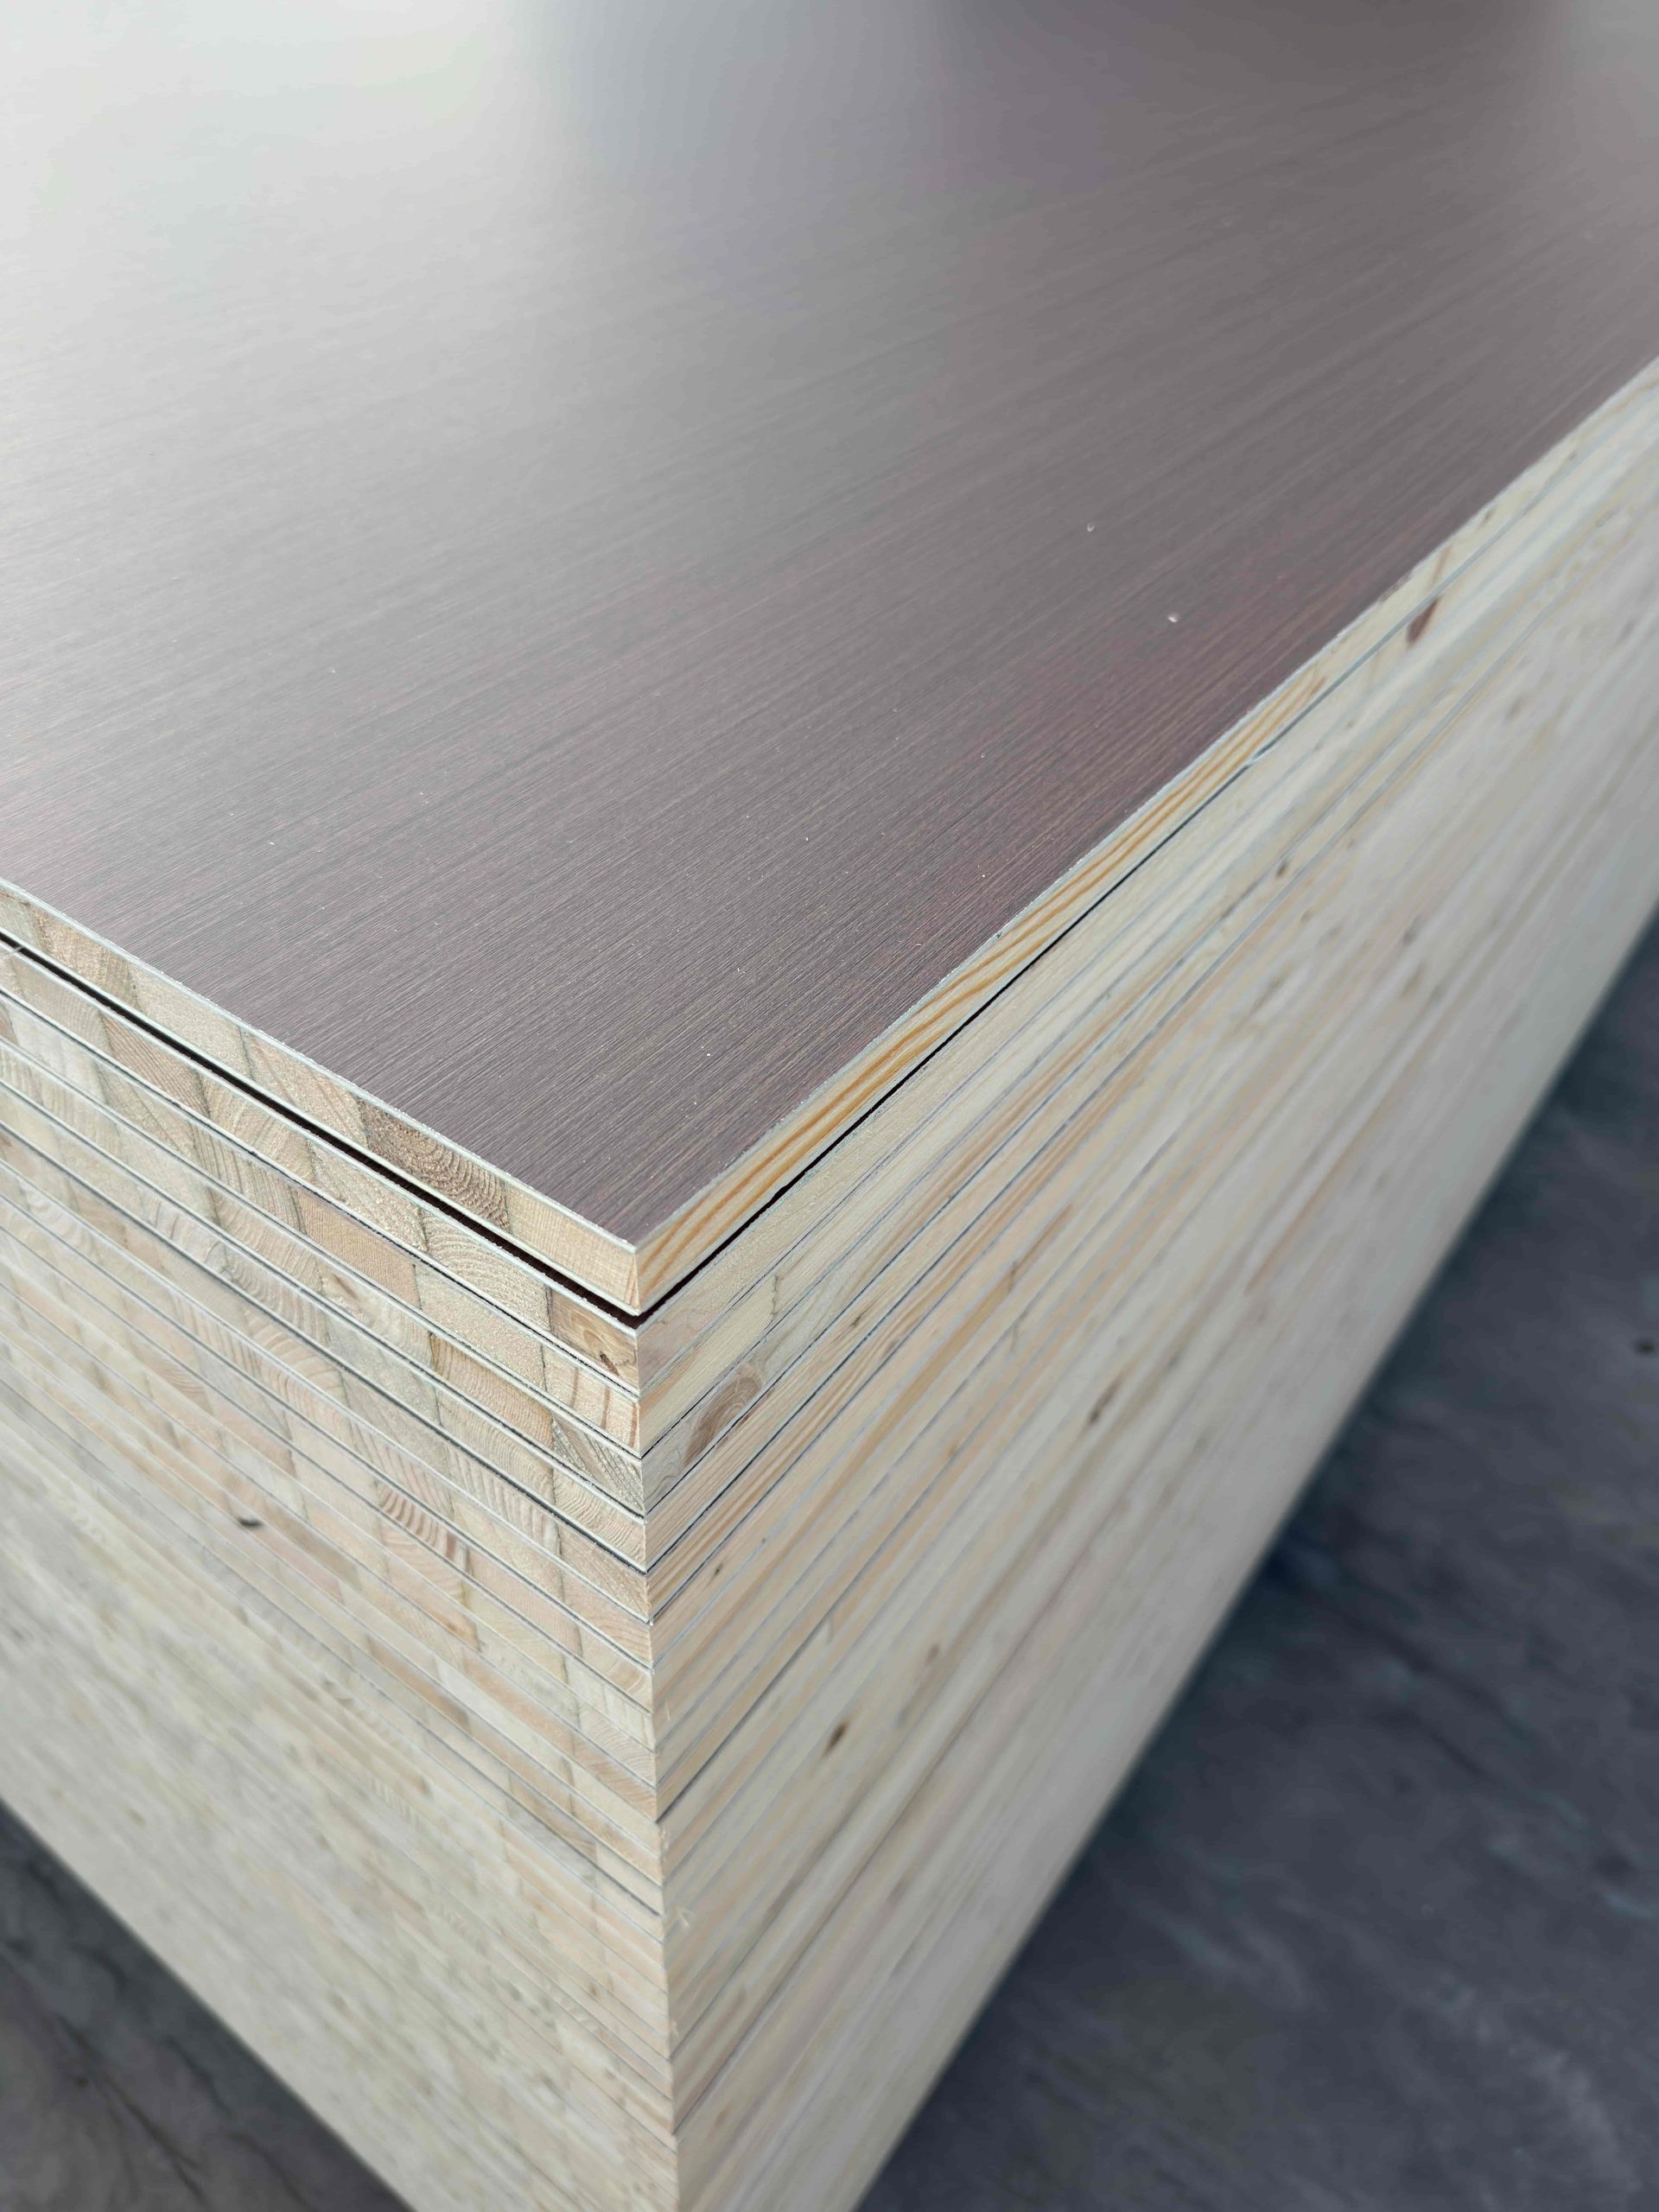
Two wardrobe panels can carry the same white or woodgrain melamine surface and still behave very differently in production. One may be melamine-faced blockboard; the other may be melamine-faced chipboard, usually shortened to MFC. The surface can make them look interchangeable, but the core changes weight, edge machining, fastening, flatness and the way a complaint develops.
The practical answer is not that one board is always better. In a melamine blockboard vs MFC decision, blockboard is often considered when lower panel weight, long-panel stiffness or fastening into timber strips matters. MFC is usually easier to standardize for cabinet carcasses, shelves and repeatable volume production. The wrong choice can show up later as hinge movement, visible core lines, chipped edges, shelf deflection or slow-moving inventory.
Key takeaways:
1. Specify the melamine surface and the substrate as two separate systems.
2. MFC usually gives more uniform machining and simpler volume purchasing.
3. Melamine blockboard can reduce weight and provide solid-timber fixing zones, but core layout and face construction must be controlled.
4. A wardrobe door, long shelf and cabinet side do not need the same board.
5. Approve a full specification and a cut cross-section, not only a decor sample.
The Short Answer: Choose by Component, Not by Wardrobe
A wardrobe is not one application. It contains tall doors, cabinet sides, fixed shelves, adjustable shelves, partitions, drawer parts, backs and fastening zones. Each component puts a different demand on the board. A buyer who chooses one substrate for the whole wardrobe may simplify purchasing, but can also pay for unnecessary weight or accept avoidable performance risk.
Start with the component and the failure you need to avoid. Use the melamine board system to define decor, texture, gloss and face configuration. Then select the core separately. For melamine blockboard, review strip-core construction and face build-up through the Blockboard product route. For MFC, define the particleboard grade, density profile and surface through the Particleboard product route.
| Wardrobe component | Melamine blockboard may fit when | MFC may fit when | Main check |
| Tall swing door | Lower weight and timber fixing zones are valuable | Door size is moderate and hinge design is proven | Panel flatness, weight and hinge test |
| Cabinet side | Long, narrow panels need lower weight or stiffness in one direction | Standardized CNC and system holes drive production | Thickness, hole quality and assembly square |
| Fixed shelf | The strip direction supports the span and edge finish is controlled | Span and load remain within the chosen thickness and grade | Loaded sample or agreed span rule |
| Adjustable shelf | Reduced handling weight is important | Consistent pins, drilling and repeat orders matter most | Edge distance and shelf-pin test |
| Drawer part | Rarely justified unless a special fixing need exists | Standard thickness and repeat machining suit volume work | Weight, groove quality and edge banding |
| Back panel | Usually unnecessary | Thin particleboard may still be heavier than alternatives | Use a purpose-selected thin panel instead |
What the Melamine Surface Does – and Does Not Do
Melamine decorative paper gives colour, pattern, texture and a ready-to-clean face after short-cycle pressing. It does not turn the core into another material. A smooth white face does not prove that the blockboard has tight core strips, and a woodgrain MFC surface does not prove strong edges or good fastener holding.
The European Panel Federation defines particleboard as wood particles bonded under heat and pressure, and notes its widespread use in kitchen and bedroom furniture. Its particleboard overview also explains that specific grades can be produced for moisture resistance or higher mechanical performance. Those properties must be ordered; they do not come from the decor paper.
For blockboard, the core remains a set of timber strips covered by one or more panel or veneer layers before the decorative surface is pressed. Strip species, width, moisture, joints, gaps and the thickness of the covering layers all affect the finished panel. The visible melamine face can hide these variables, so a cross-section sample is more useful than a face-only sample.
Weight Changes More Than Freight Cost
Wardrobe buyers often compare board weight only because it changes container payload. In use, weight also changes door handling, hinge load, installation effort and the force on a tall cabinet during movement. A heavy panel is not automatically stronger, and a light panel is not automatically weak.
MFC weight is influenced by particleboard density, moisture, actual thickness and sheet size. Melamine blockboard weight is influenced by timber species, strip size, moisture, face build-up and void content. Therefore, compare approved full-sheet weights only after actual dimensions and moisture condition are reasonably consistent.
A practical weight check for small buyers
- Measure the actual length, width and thickness before comparing sheet weight.
- Weigh sheets from several bundles, not only one convenient top sheet.
- Record whether the sample is raw, one-side faced or two-side faced.
- Cut and keep a labelled cross-section from each approved construction.
- Test the real door size with the planned hinges before approving mass production.
The USDA Forest Service Wood Handbook treats fastenings, panel products, moisture and mechanical properties as related design subjects. That is the right way to think about a wardrobe door: board weight, fastener location and moisture condition must be considered together.
Flatness and Door Stability Are Separate Questions
A sheet can be flat when it leaves the press and still move after cutting, storage or installation. Decorative paper on both faces helps balance surface stresses, but it cannot correct an unstable core. Melamine blockboard is especially sensitive to core-strip moisture differences, gaps and unbalanced face construction. MFC can also warp when density, moisture, stacking or one-sided surface treatment is uneven.
Wood exchanges moisture with surrounding air. The USDA Forest Service chapter on drying and moisture control explains that correct drying, handling and storage reduce dimensional changes. This matters because a blockboard core contains timber strips that can respond directionally to moisture changes. It also matters for MFC because exposed edges and drilled holes remain paths for moisture.
Do not approve a tall wardrobe door from a small hand sample. Produce a full-size trial door with the planned height, width, hinge quantity, edge band and handle position. Store it vertically and horizontally under normal factory conditions, then check twist, bow and hinge alignment before confirming the order.
Fastening: Solid Timber Helps Only Where the Screw Lands
Blockboard can offer useful fastening when a screw enters a sound timber strip. That advantage disappears when the fixing lands on a core gap, a weak joint or a poorly supported edge. Core-strip direction and the expected hinge zone should therefore be shown on the sample and production drawing.
MFC gives a more uniform particle structure, but fastener performance depends on the face and core density, hole diameter, edge distance, insertion depth and assembly torque. The article on cam-lock breakout in particleboard shows why the real joint geometry is a better approval test than one isolated screw pull in the centre of a sheet.
| Fastening risk | Melamine blockboard | MFC | Buyer action |
| Hinge screw near edge | Strong if it enters a sound strip; inconsistent if it meets a gap | More uniform but sensitive to edge distance and core density | Drill the production hinge pattern in a full-size door |
| System-hole drilling | Core changes can affect exit quality | Usually more predictable for line boring | Inspect entry and exit edges across several sheets |
| Repeated assembly | Timber strip may hold well if the same hole is not damaged | Repeated removal can enlarge particle-based holes | Run at least two assembly cycles with actual hardware |
| Narrow cut component | May expose joints or unsupported face layers | Can chip if the surface layer is brittle or tools are dull | Cut the narrowest production part during sample approval |
Machining and Edge Banding Can Reverse the Cost Advantage
MFC is widely used in panel furniture because its structure is compatible with repeatable cutting, drilling and edge-banding lines. Melamine blockboard may reduce weight, but its edge can expose timber-strip joints and local voids. If the buyer needs extra filling, wider trimming or a thicker edge band, the lower sheet price may not become a lower finished-part cost.
Use the customer’s real saw, feed speed and edge-banding setup during approval. Check both long-grain and cross-grain cuts on blockboard. On both products, inspect the melamine surface for entry and exit chipping, then look at whether the exposed core supports a continuous glue line.
Do not compare only price per sheet. Compare usable cutting yield, machining speed, rejected parts, edge-band consumption, hardware performance, door weight, packing density and repeat-order stability. A panel that saves USD 1 per sheet can still be the more expensive choice if it creates rework or slow furniture assembly.
Moisture Risk Starts at Edges, Holes and Storage
Standard melamine-faced panels should not be sold as waterproof. The face slows direct wetting, while cut edges, hinge cups, shelf holes and damaged corners remain exposed. A moisture-resistant particleboard grade can reduce risk in an appropriate humid interior application, but it still needs correct edge treatment. Blockboard also needs a core moisture condition suitable for the destination and stable protective packing.
For import orders, ask for protected faces, corner guards, a stable pallet or runner layout, moisture protection appropriate to the route and clear bundle labels. On arrival, photograph the container before unloading, check wet packaging, keep panels off the floor and allow the boards to reach the workshop condition before immediate full-scale cutting.
What to Put in the RFQ and Purchase Contract
The phrase “18 mm woodgrain melamine board” is not a complete specification. It leaves the substrate, actual thickness, reverse face, core quality and intended component open to interpretation. Use one line item per construction and keep the same identity on the quotation, approved sample, bundle label and packing list.
| Specification field | Melamine blockboard | MFC |
| Finished size and thickness | Nominal and accepted tolerance after facing | Nominal and accepted tolerance after facing |
| Core identity | Timber species or agreed construction, strip direction and gap expectation | Particleboard grade, density or agreed performance requirements |
| Face build-up | Covering-layer construction and preparation before pressing | Sanding and surface condition before pressing |
| Decorative surface | Decor code, texture, gloss, one- or two-side configuration | Decor code, texture, gloss, one- or two-side configuration |
| Application | Door, long shelf, cabinet side or other named part | Carcass, shelf, drawer, door or other named part |
| Approval evidence | Face sample, labelled cross-section and full-size critical component | Face sample, cut edge and hardware test part |
| Packing | Sheet count, protection, runners, straps and marks | Sheet count, protection, runners, straps and marks |
Momentimber can coordinate specification matching, sample confirmation, production follow-up, inspection and packing across different panel categories through its wood-panel sourcing process. The useful starting point is the wardrobe component, size, decor, hardware and destination environment, not a generic request for the “best board.”
A Simple Pre-Shipment Inspection Plan
- Identity: confirm substrate, size, thickness, decor, texture, face configuration and bundle code.
- Cross-section: cut samples from several sheets and compare the approved core construction.
- Dimensions: measure thickness at multiple edge and centre points and check diagonals.
- Flatness: inspect sheets on a stable support and assemble at least one critical full-size component.
- Machining: cut, drill and edge-band with the buyer’s production settings or an agreed equivalent.
- Fastening: install the actual hinge, cam or shelf fitting at the real edge distance.
- Surface: compare colour and texture beside the retained Golden Sample under the same light.
- Packing: record bundle count, protection, labels, container condition and loading sequence.
This plan does not require expensive laboratory equipment. It requires a retained sample, a caliper, a straight reference, a scale where practical, ordinary production tools and disciplined photos. Laboratory or third-party testing can be added when the contract or destination regulation requires it.
Melamine Blockboard vs MFC: Final Decision
The melamine blockboard vs MFC choice should follow the wardrobe component. Choose MFC when the priority is standardized panel-furniture production, repeatable drilling, familiar edge banding and a broad commodity supply base. Consider melamine blockboard when lower panel weight, long narrow components or fastening into timber strips offers a clear benefit and the supplier can control the core, face build-up and flatness.
Do not force one substrate into every wardrobe component. A controlled two-board range can be safer than one “universal” board if the SKU volume remains manageable. The winning specification is the one that your customer can machine, assemble and reorder consistently.
FAQ
Related Reading
Sanded OSB for Furniture Still Needs a Finish Plan
OSB material reference only; sanding quality and the final finish need separate approval. Sanded OSB…
Plywood vs OSB for Crates Is More Than a Price Choice
Protected panel bundles are a supply-stage reference, not an approved design for a shipping crate….
Blockboard vs Finger Joint Board for Furniture Buyers
A visible timber-strip core does not make the finished panel the same as an exposed…
Synchronized Melamine Board Goes Beyond the Print
Woodgrain design reference only. A flat image cannot demonstrate EIR texture or alignment. Synchronized melamine…
Lightweight MDF vs Standard MDF for Furniture Parts
Panel appearance alone does not identify a lightweight MDF grade. Lightweight MDF can make a…
Film Faced Plywood Edge Sealing After Cutting
Film faced plywood edge sealing needs to follow the cutting and drilling plan. Factory edge…
Evaluate the Order, Not Just the Factory
Send the intended application, plywood construction, target market, quantity and the evidence you already have. We can help turn those requirements into a supplier comparison, sample checklist and inspection plan.